Water Treatment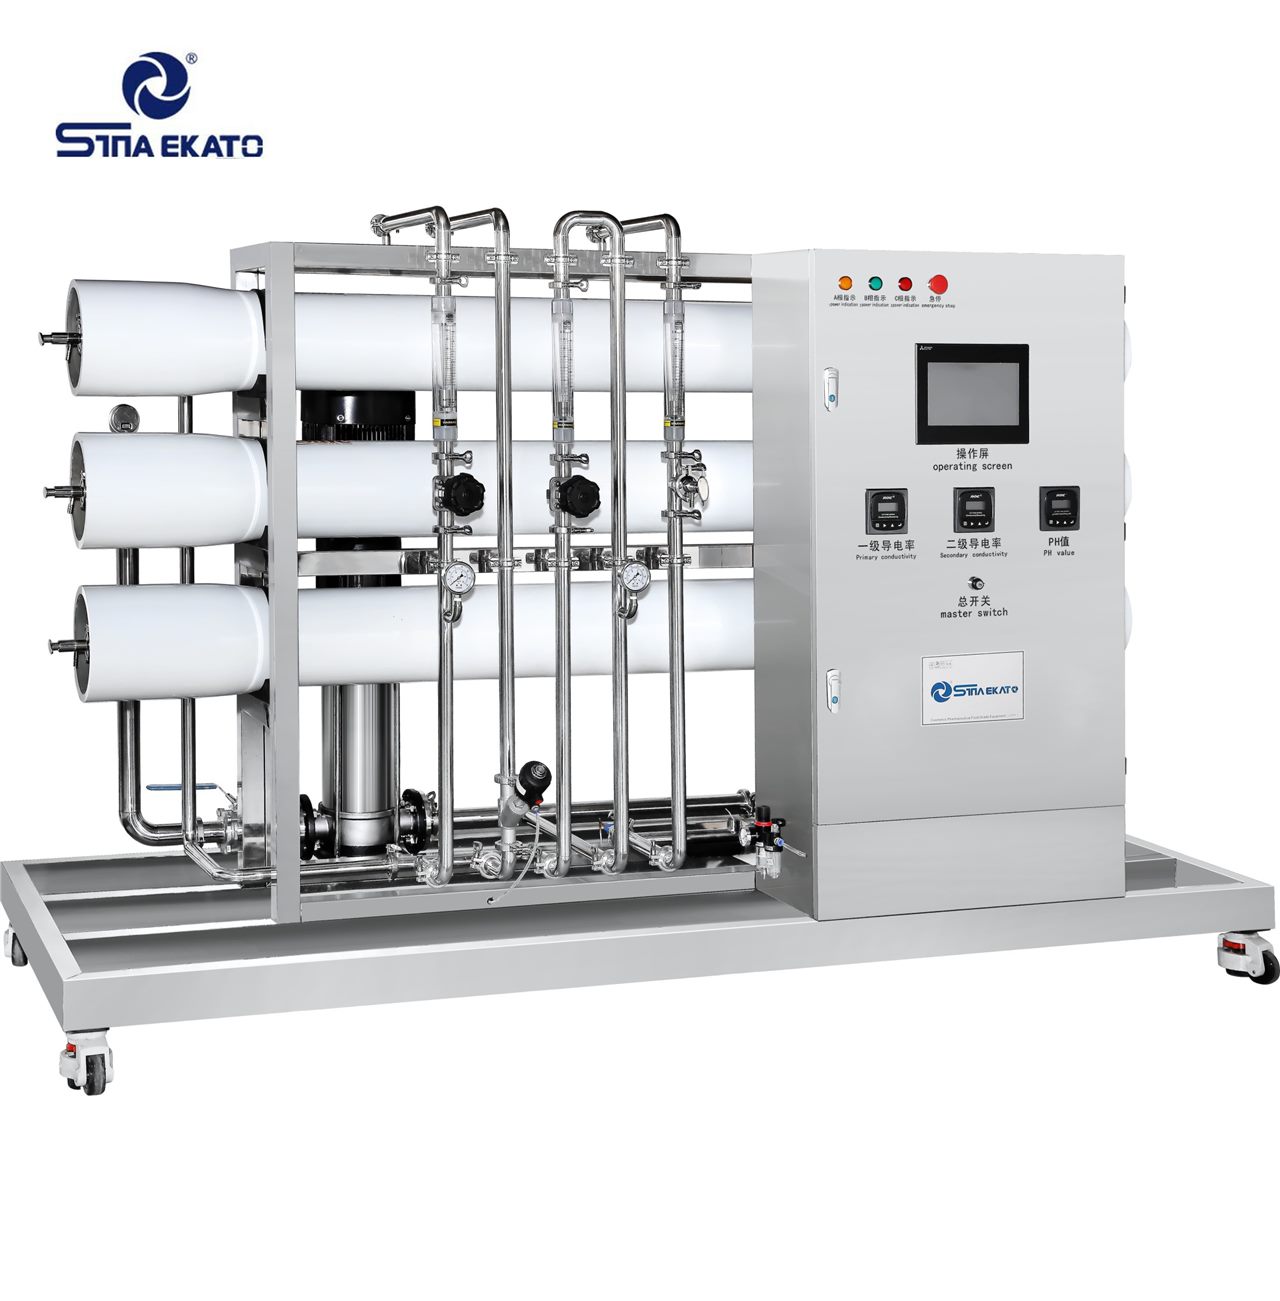
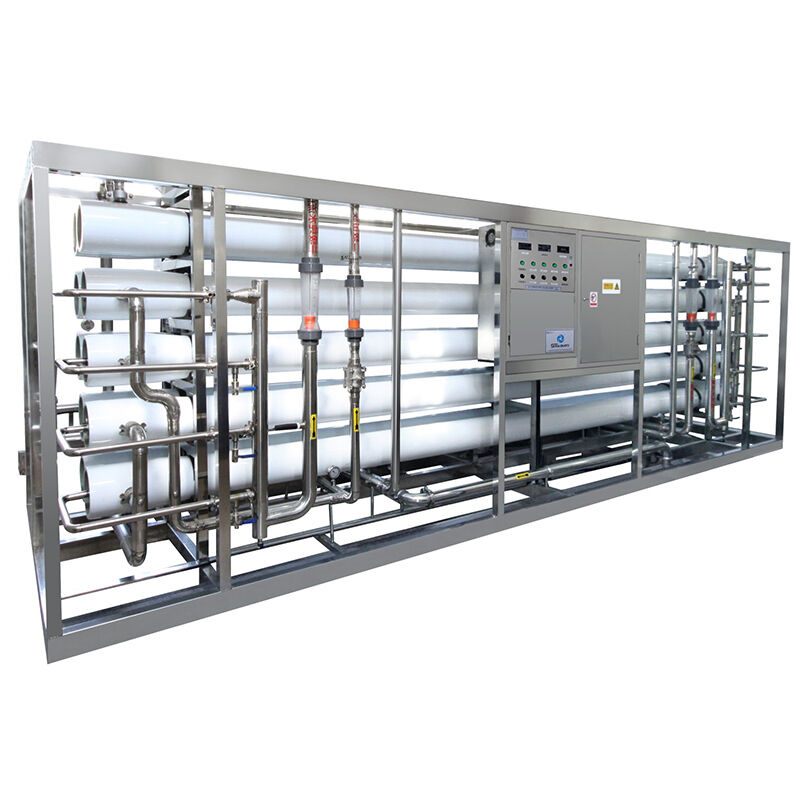
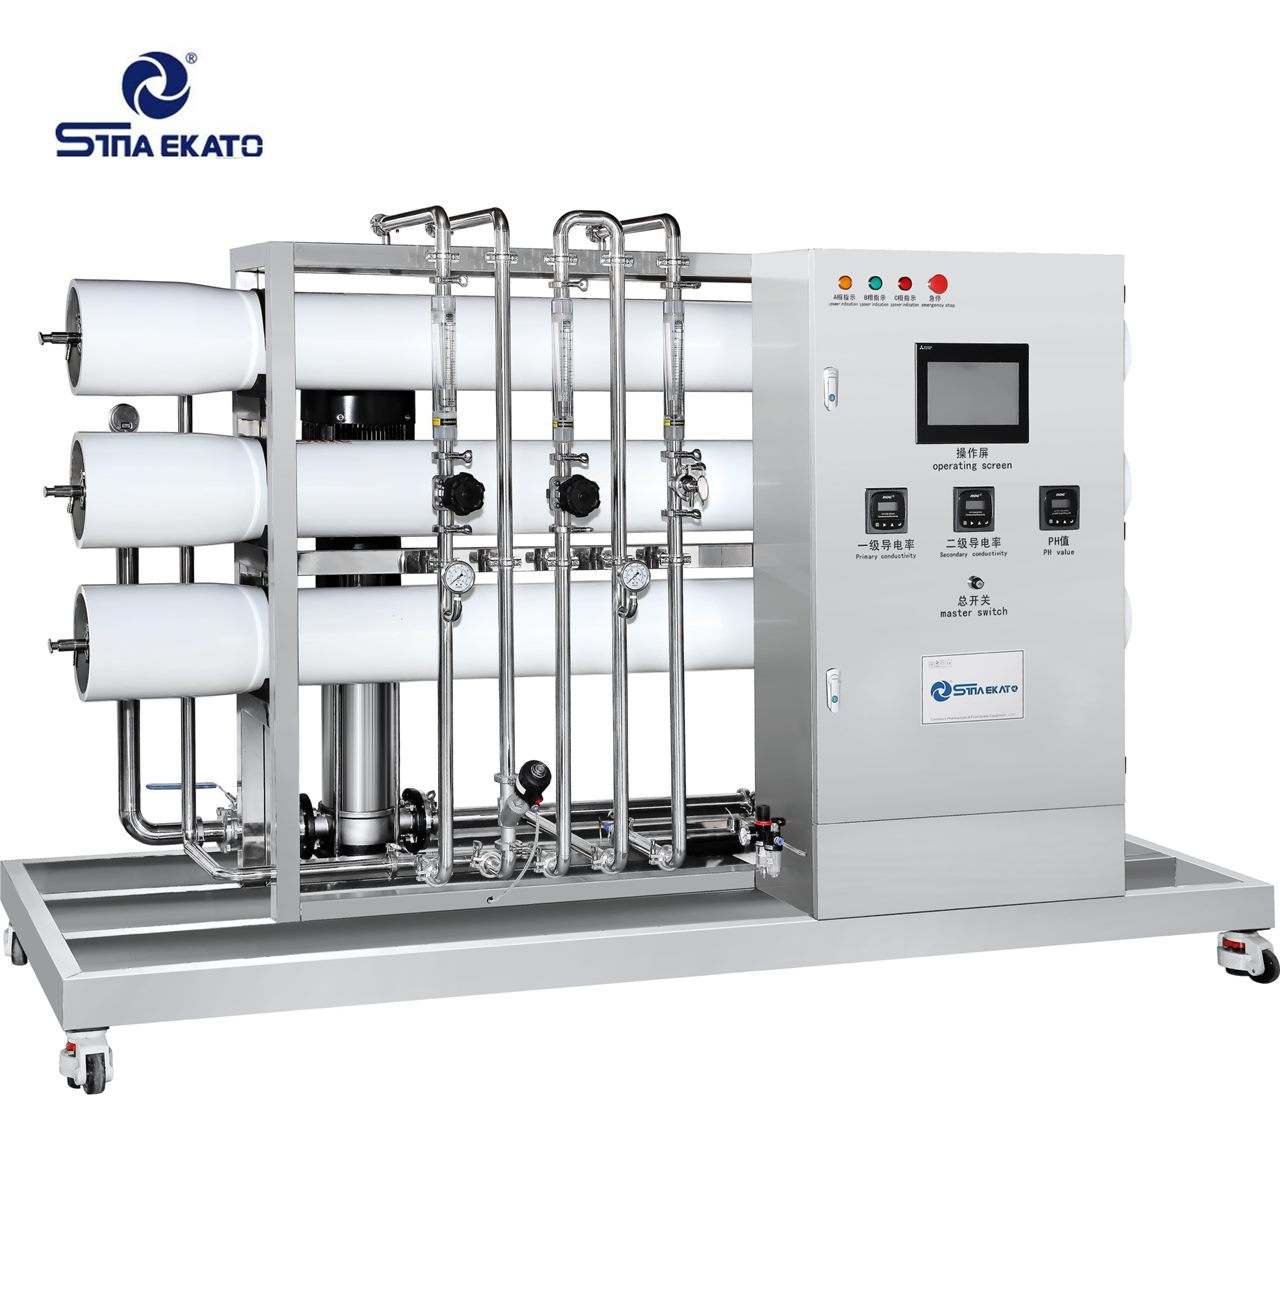
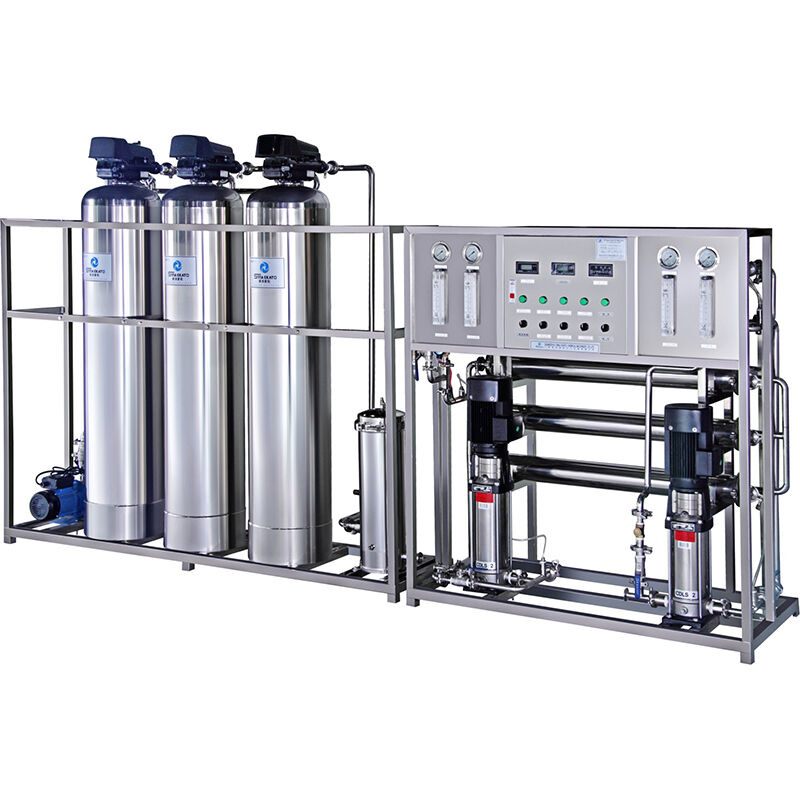
Reverse Osmosis Water Treatment System (0.5–20 T/H)
Reverse osmosis purification plant producing high-purity process water for cosmetics, pharmaceuticals and food — from 0.5 to 20 T/H.
View machine
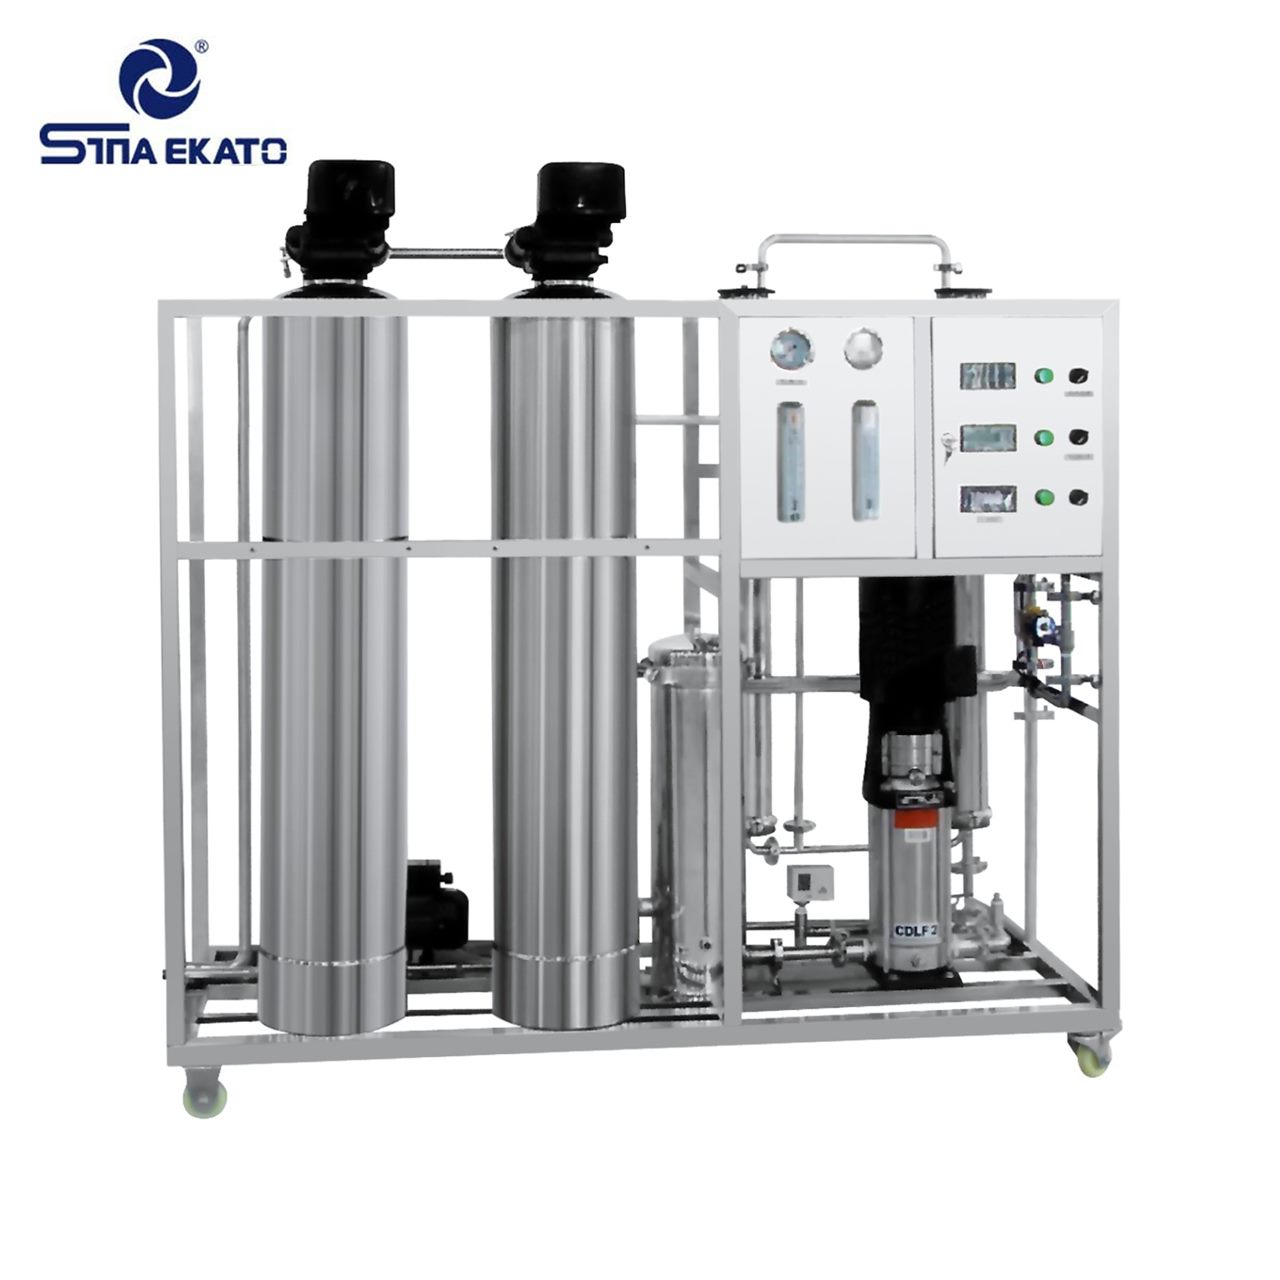
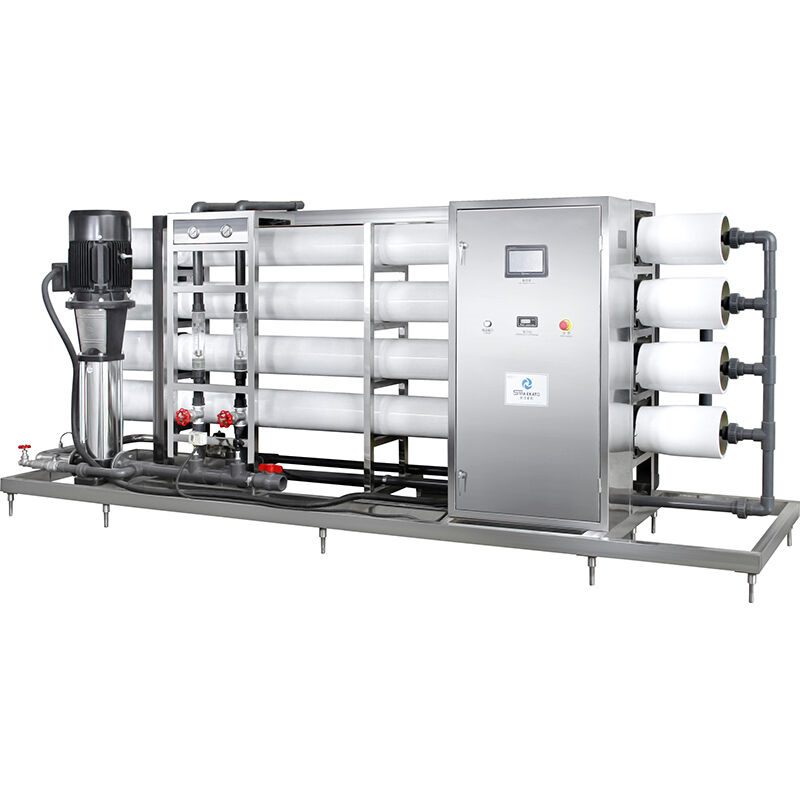
Raw Water Pretreatment Unit, High-Pressure Pump Unit, RO Membrane Module Unit
| Place of origin | Jiangsu China |
|---|---|
| Brand | SINA EKATO |
| Model series | RO |
| Certification | ISO9001, CE |
| Minimum order | 1 Set |
| Delivery | 30-40 working days |
| Packaging | Standard Export Wooden Case |
| Payment terms | T/T, L/C, |
· Alternative Names: RO Water Purifier, Industrial Water Treatment Plant, Pure Water System, Reverse Osmosis Filtration.
The pre-treatment is the foundational guarantee to protect the reverse osmosis membrane and ensure the stable operation of the whole system, which is used to remove suspended solids, turbidity, residual chlorine, colloids, iron and manganese ions from raw water. Common equipment includes quartz sand filters, activated carbon filters, precision filters (5μm/1μm), softeners, and anti-scaling dosing devices. This unit effectively prevents membrane fouling, oxidation, and physical damage, extending the service life of the RO membrane.
As the power core of the RO system, the high-pressure pump provides a stable and adjustable working pressure that meets the reverse osmosis process requirements (the working pressure is usually 1.0-4.0MPa for brackish water desalination, and 5.0-8.0MPa for seawater desalination). It adopts industrial-grade high-pressure centrifugal pumps or plunger pumps with high efficiency, low noise, and stable operation, equipped with pressure protection devices to avoid system damage caused by overpressure or underpressure.
The core separation component of the system, the RO membrane module is usually composed of spiral-wound composite membranes (the most widely used type in the industry) and pressure vessels. The spiral-wound composite membrane has the advantages of high water production flux, high salt rejection rate, and good chemical stability. Membrane modules are configured in parallel/series according to water production capacity, and the common membrane specifications include 4-inch and 8-inch. The salt rejection rate of industrial-grade RO membranes can reach more than 98%, and the removal rate of bacteria, viruses, and heavy metals is close to 100%.
This unit is responsible for the collection, transportation, and pressure regulation of the purified product water and the discharged concentrated water. It is equipped with product water tanks, pressure gauges, flow meters, and concentrated water regulating valves. The concentrated water regulating valve can adjust the recovery rate of the system (the water recovery rate of industrial RO systems is usually 70-85%) according to the actual working conditions, and the concentrated water can be recycled or discharged up to standard after secondary treatment to realize water resource utilization.
Including cleaning water tank, cleaning pump, chemical dosing device, and cleaning pipeline, it is used for online/offline chemical cleaning of the RO membrane module. After long-term operation, the membrane surface will produce organic/inorganic fouling and microbial adhesion, leading to the decrease of water production flux and salt rejection rate. Regular cleaning with acid/alkali cleaning agents (such as citric acid, sodium hydroxide) can restore the membrane performance and ensure the long-term stable operation of the system.
Adopts PLC (Programmable Logic Controller) + touch screen integrated control system, which can realize automatic start and stop of the whole system, real-time monitoring of key parameters (inlet/outlet pressure, water production flow, conductivity, pH value), automatic alarm and protection of abnormal conditions (overpressure, low flow, high conductivity), and automatic backwashing of pretreatment equipment. The system supports manual/auto switching, with high automation degree, reducing manual operation and management costs.
: The salt rejection rate is over 98%, and it can effectively remove heavy metal ions (e.g., lead, mercury, chromium), bacteria, viruses, organic matter, and colloids in water, with the purified water conductivity as low as 1-10μS/cm (pure water) or even lower (ultra-pure water after secondary treatment).
: No chemical additives are needed in the core purification process, avoiding secondary pollution of water quality, and the product water quality is stable and reliable without chemical residues.
: It can handle various raw water sources, including tap water, groundwater, surface water (river water, lake water), brackish water, and seawater, and is suitable for different water treatment scenarios such as desalination, purification, and wastewater reuse.
: The integrated automatic control system realizes unmanned operation under normal working conditions, with real-time data display and fault alarm, and the daily maintenance is simple and convenient.
: The modular design of the system saves installation space, and the concentrated water can be recycled, which improves the utilization rate of water resources; the core equipment (high-pressure pump, membrane module) adopts energy-saving models, reducing the overall energy consumption of the system.
: The key components are made of industrial-grade corrosion-resistant and high-pressure resistant materials (e.g., stainless steel, FRP), with a long service life; the system has a perfect protection mechanism, which can adapt to the fluctuation of raw water quality and working conditions, and the operation is stable and reliable.
: Production of pure water/ultra-pure water for raw material preparation, reaction kettle cooling, pharmaceutical injection, and cosmetic production (e.g., lotion, shampoo, skin care products), meeting the GMP and industrial production water quality standards.
: Purification of production water for detergents, surfactants, and personal care products, avoiding the impact of impurities in water on product quality and performance.
: Production of ultra-pure water for semiconductor manufacturing, circuit board cleaning, and electronic component processing, with strict requirements for water conductivity and impurity content.
: Pure water for beverage production, wine brewing, and dairy product processing, ensuring food safety and product taste.
: Desalination and purification of industrial wastewater (e.g., chemical wastewater, printing and dyeing wastewater), realizing the recycling of water resources and reducing environmental pollution and water resource consumption.
: Drinking water purification in residential areas, commercial plazas, and hotels, especially in areas with high groundwater salinity or poor surface water quality.
: Boiler make-up water purification for thermal power plants and nuclear power plants, avoiding boiler scaling and corrosion caused by impurities in water.
Regularly monitor the key parameters of the system (inlet pressure, water production flow, conductivity, concentrated water ratio) and record the data to track the operation status of the membrane module.
| Model RO-500 | Capacity (T/H) 0.5 | Power (KW) 0.75 | Recovery Rate (%) 55-75% | One Stage Conductivity ≤10μs/cm | Two Stage Conductivity 2-3μs/cm |
|---|---|---|---|---|---|
| RO-1000 | 1.0 | 2.2 | 65-75% | ≤10μs/cm | 2-3μs/cm |
| RO-2000 | 2.0 | 4.0 | 65-75% | ≤10μs/cm | 2-3μs/cm |
| RO-5000 | 5.0 | 7.5 | 65-76% | ≤10μs/cm | 2-3μs/cm |
| RO-10000 | 10.0 | 11.0 | 65-76% | ≤10μs/cm | 2-3μs/cm |
Reverse osmosis purification plant producing high-purity process water for cosmetics, pharmaceuticals and food — from 0.5 to 20 T/H.
View machine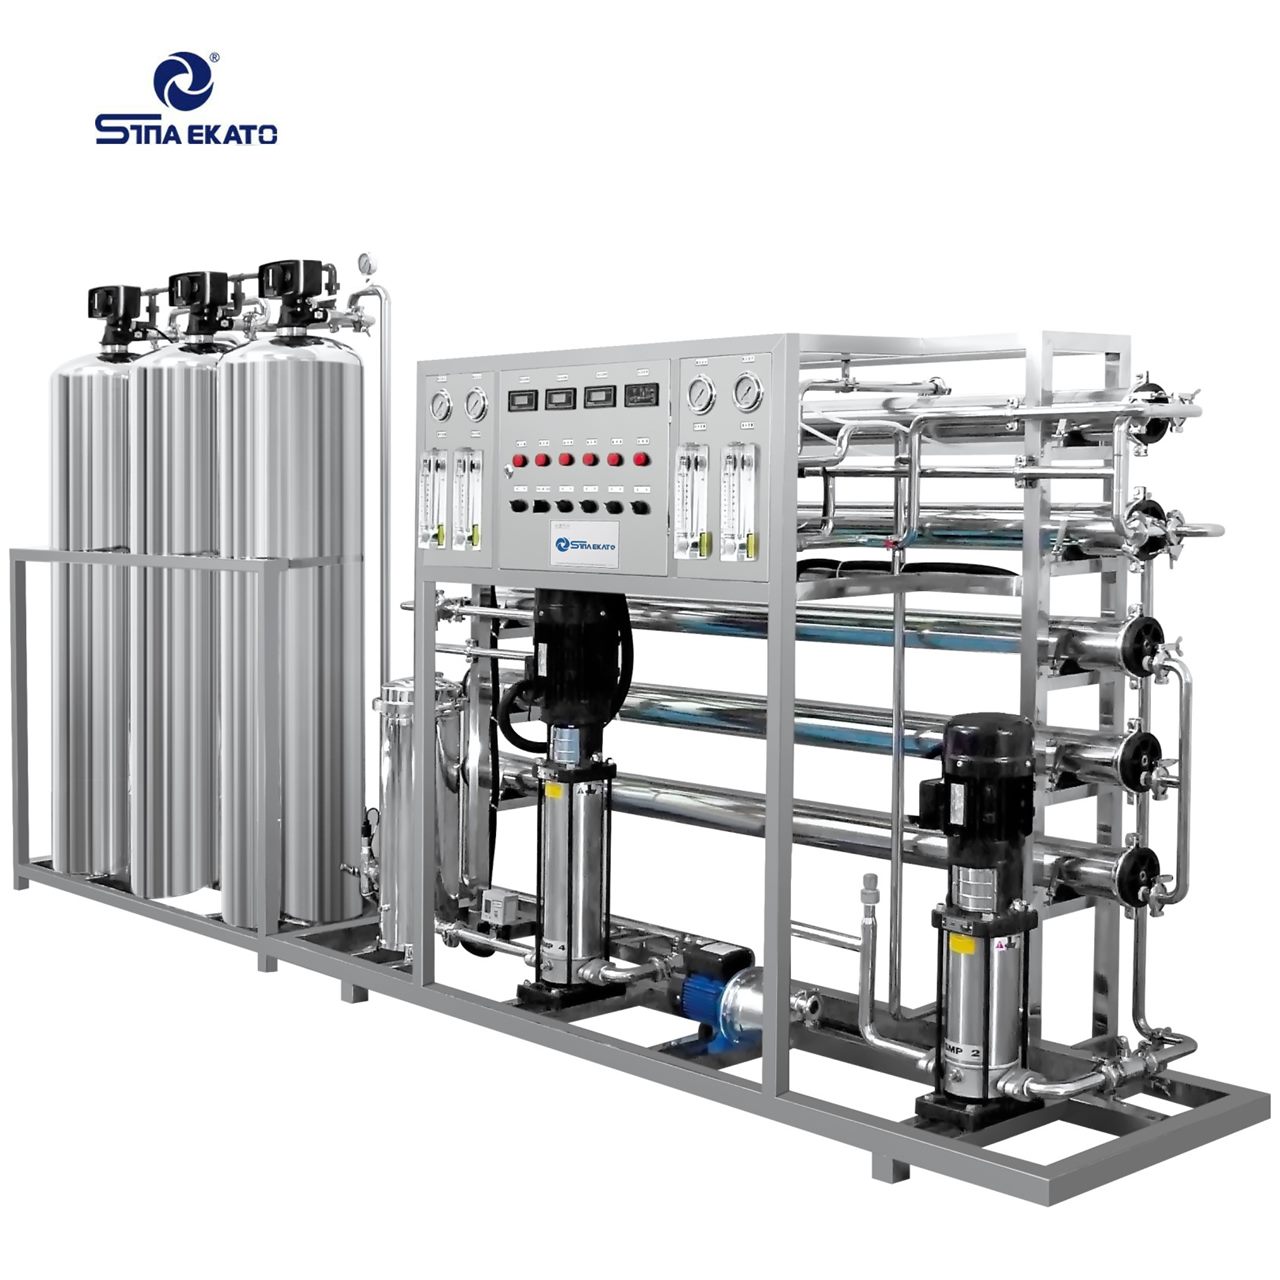
· Alternative Names: RO Water Purifier, Industrial Water Treatment Plant, Pure Water System, Reverse Osmosis
View machine
Hydraulic-lifting vacuum emulsifying mixer with high-shear homogenizer, 316L contact parts and PLC touch-screen control for cream and lotion production.
View machineSend us your product, target capacity and workshop layout — our engineers will reply with a tailored equipment proposal and quotation.
Tell us your product and capacity needs — our engineers reply with a tailored proposal. Your default email app will open with the message prepared.